Custom Liquid Cooling Connectors for Cold Plates
Date:2026-09-30Article editor:Starting Point PrecisionViews:230As power densities rise in data centers, electric vehicles, and industrial power electronics, cold plate liquid cooling has become the preferred thermal management method. At the heart of every reliable cold plate loop sits a component often overlooked until it fails: the custom liquid cooling connector.
This guide explores how custom connectors are engineered, what to specify, and how to avoid common pitfalls.
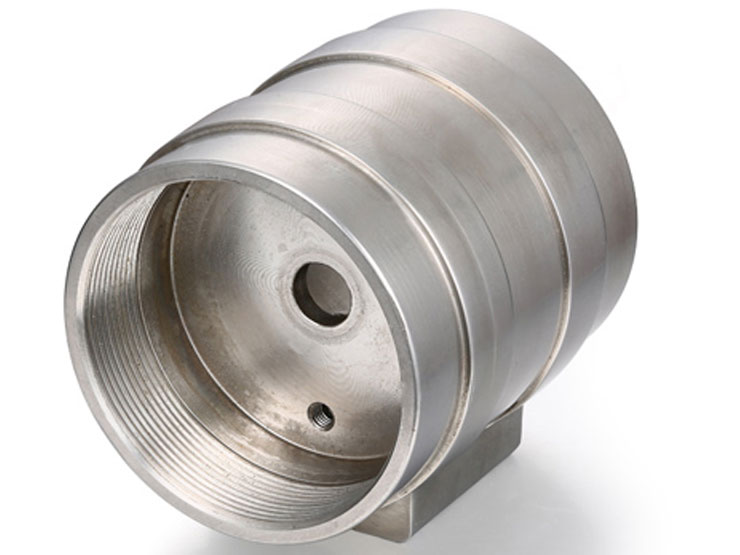
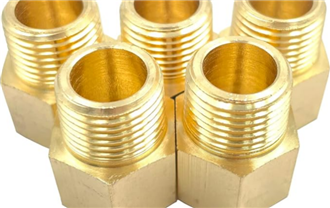
Custom liquid cooling connectors are purpose-built fluid couplings designed to mate with cold plates, manifolds, and heat exchangers. Unlike off-the-shelf fittings, they are tailored to specific flow rates, pressure drops, tube sizes, and spatial constraints.
They typically serve three functions:
• Leak-free connection under thermal cycling and vibration
• Quick disconnect for serviceability
• High flow with low pressure drop to maximize cooling efficiency
When specifying custom connectors for cold plates, engineers evaluate several parameters:
| Parameter | Why It Matters | Typical Range |
| Flow rate | Determines cooling capacity | 0.5–20 L/min |
| Operating pressure | Prevents burst or leakage | 1–10 bar |
| Temperature range | Material compatibility | -40°C to 150°C |
| Material | Corrosion, weight, cost | Brass, stainless steel, aluminum, engineering plastics |
| Connection type | Ease of assembly | Push-to-connect, threaded, flanged |
| Seal material | Chemical compatibility | EPDM, FKM, silicone |
The choice of material directly impacts durability and thermal performance. Stainless steel offers excellent corrosion resistance for deionized water loops, while aluminum reduces weight in automotive cold plates. Engineering plastics such as PPS or PA66 provide cost-effective solutions for lower-pressure applications.
Precision machining is critical. Tolerances on the order of ±0.05 mm ensure proper sealing and mating. For high-volume production, CNC machining, injection molding, and die casting are common processes. Working with an experienced manufacturing partner—such as Start Precision—can streamline prototyping through production.
Reliable connectors undergo rigorous validation:
• Helium leak testing to detect micro-leaks
• Pressure cycling (e.g., 10,000 cycles)
• Thermal shock from -40°C to 125°C
• Vibration testing per IEC 60068
Industry leaders like CPC (Colder Products Company) and Staubli set benchmarks for quick-disconnect reliability.
• Data center servers: Direct-to-chip cooling with blind-mate connectors
• Electric vehicles: Battery cold plates and power electronics
• Medical devices: MRI and laser cooling
• Aerospace: Avionics thermal management
Before finalizing a custom connector design, confirm:
□ Compatible with coolant chemistry
□ Meets pressure and temperature ratings
□ Fits envelope and mating constraints
□ Supports required flow rate at acceptable pressure drop
□ Passes leak and cycle testing
□ Available in required production volumes
Custom liquid cooling connectors are small components with an outsized impact on cold plate performance. By understanding flow, pressure, material, and sealing requirements, engineers can specify connectors that deliver years of reliable service.
Contact us to discuss your manufacturing needs. Our team supports connector design, prototyping, and volume production for cold plate cooling systems worldwide.
Q1: What is the best material for a liquid cooling connector?
A: It depends on the coolant and environment. Stainless steel suits deionized water; aluminum works for weight-sensitive EV applications; engineering plastics are cost-effective for low-pressure loops.
Q2: How do I prevent leaks in cold plate connectors?
A: Use high-quality seals (EPDM, FKM), validate with helium leak testing, and account for thermal expansion in the design.
Q3: Can custom connectors handle high flow rates?
A: Yes. Custom designs can achieve 20+ L/min with minimal pressure drop by optimizing internal geometry.
Q4: What is the typical lead time for custom connectors?
A: Prototyping can take 2–4 weeks; production timelines depend on volume and process (CNC, molding, casting).
Q5: Are quick-disconnect connectors reliable?
A: Reputable quick-disconnects are rated for thousands of cycles. Choose connectors tested to industry standards like IEC 60068.
Add: Building 3No.277 Zhen'an Middle Road, Chang'an Town,Dongguan,Guangdong, China
Tel:+86-769-82855591
Copyright © 2019 All Rights Reserved Dongguan Start Precision Technology Co., Ltd. Tel: +86-769-82855591
Add: No. 277 Zhen'an Middle Road, Chang'an Town, Dongguan, Guangdong, China
 中文版
 English